


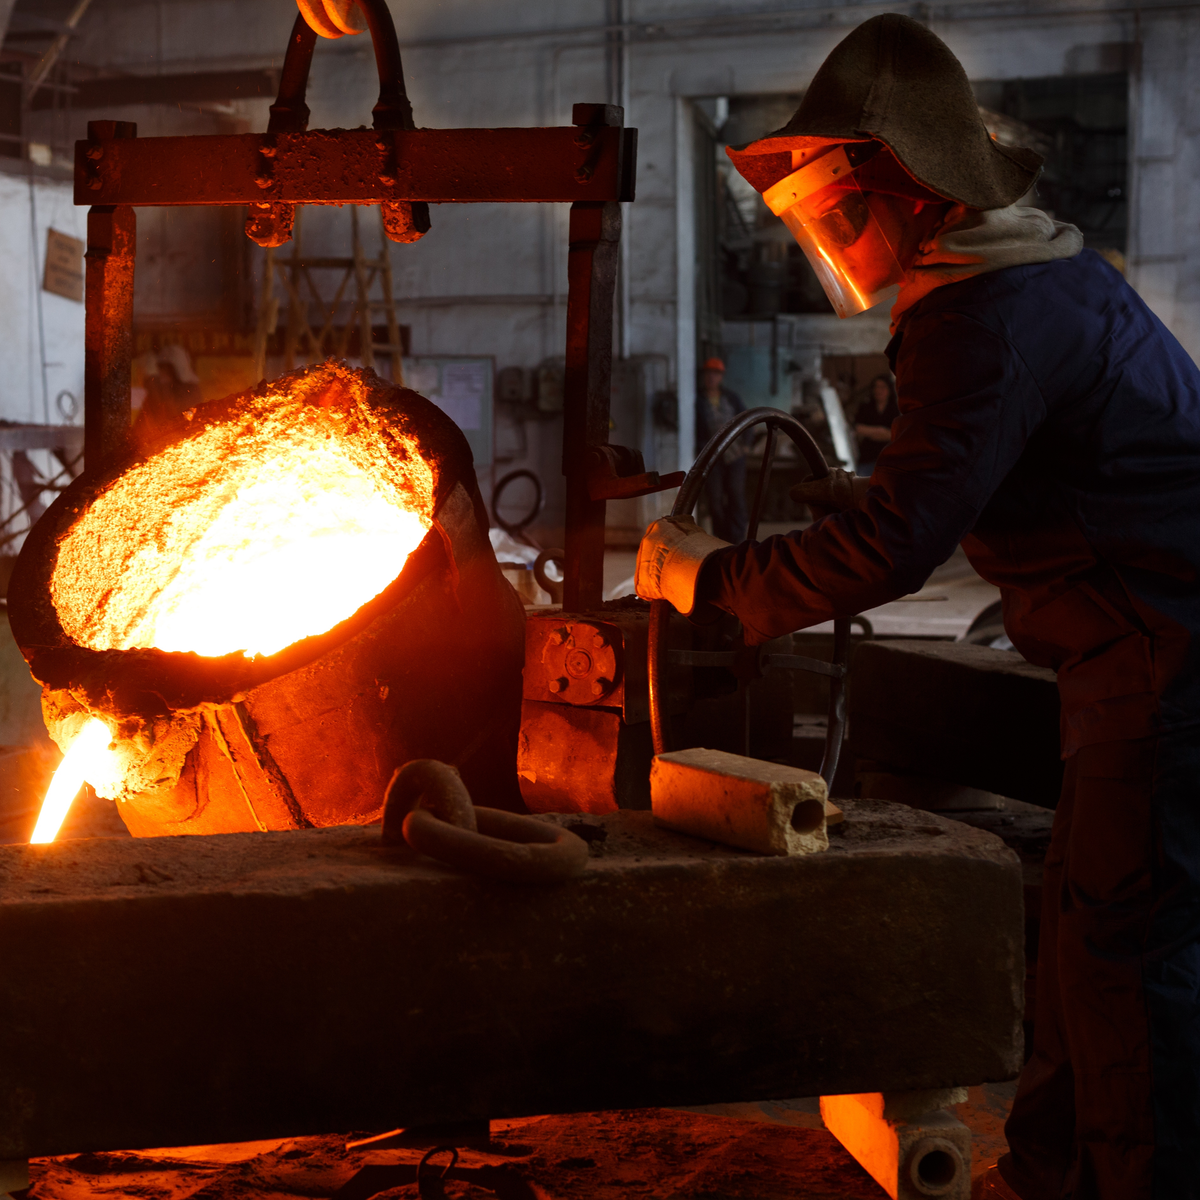
Ask a foundry maintenance guy what kills compressors and he will not say hours. He will say sand. Every foundry compressor room eventually tells the same story: an intake filter that looks like it was pulled out of a sandbox, a cooler core packed solid with fines, and a discharge temperature that has been creeping up for two years while everybody blamed the weather.
Compressed air for foundries is not really a sizing problem. Most foundries get the CFM roughly right. It is an environment problem. You are asking a machine that wants clean, cool, dry intake air to live in a building full of airborne silica at 105 degrees.
What the Air Is Actually Doing
Foundry air does more jobs than in almost any other plant, and they pull very differently:
- Core blowing. Core blowers shoot sand into the core box at roughly 100 psi. These are short, violent, high-volume shots. A single blower can demand several hundred CFM for a second or two, many times a minute.
- Molding machines. Squeeze, jolt, draw and roll-over cylinders. Continuous cycling, moderate volume.
- Pneumatic rammers and chipping hammers. Continuous consumers in the range of 15 to 40 CFM each, and there are usually more of them running than anybody admits.
- Shot blast and cleaning room. Blast cabinets, air wands, and grinding. This is often the single largest continuous block of demand in the plant.
- Pneumatic conveying. Moving sand, dust and shot between systems.
- Shakeout and vibrators. Steady moderate draw.
- Furnace and ladle work. Actuation, plus air on some burner systems.
That mix is the sizing headache. The core blowers and the cleaning room have almost nothing in common. One is spike demand, the other is flat demand, and if you size one machine to cover both you buy far more compressor than you need and it still sags when three cores blow at once.
Storage Solves Core Blowing. Horsepower Does Not.
This is the single most useful thing to get right in a foundry.
A core blower shot is over before a compressor can respond to it. Compressors take seconds to load and come up; a blow cycle takes a fraction of a second. Buying a bigger compressor to chase core blow peaks is spending capital on a machine that will spend most of its life unloaded while the pressure still dips when the blowers fire together.
What actually works is dedicated storage close to the core room, sized on the volume of air the blowers pull per shot rather than on CFM. Put a receiver near the blowers, feed it through a restrictor so it refills gradually instead of robbing the header, and let it absorb the spike. The plant compressor then only has to cover the average.
Rule of thumb for foundries: 8 to 15 gallons of storage per CFM of average demand, and more of it distributed out toward the core room rather than all sitting in the compressor room. Our guide to air receiver tanks covers how to size and plumb them.
The Intake Air Problem
Here is where foundries lose compressors.
Your plant ambient is loaded with respirable silica, sand fines, mold binder smoke and shot dust, and it is hot. A rotary screw sitting in that room is inhaling all of it. Three things follow, in order:
- The intake filter loads fast. Not annually. In a bad foundry, monthly. A restricted intake starves the airend, drops capacity and drives discharge temperature up.
- Whatever gets past the filter goes into the oil. Abrasive fines in compressor oil are exactly what you would expect them to be: lapping compound running through bearings and rotors at 3,600 RPM.
- The cooler plugs. Air-cooled aftercoolers and oil coolers in a foundry pack up with dust on the fin face. Discharge temp climbs, the machine starts high-temp tripping in August, and somebody undersizes the problem as "it needs more ventilation."
The fix is not exotic. Duct the compressor intake to outside air, or to a filtered clean space, and stop drawing plant air. Add a pre-filter on the intake duct so you are changing a cheap panel filter instead of the compressor's element. Then put cooler cleaning on the PM schedule at an interval that matches your plant, not the manual's.
Hot ambient matters too. A compressor rated at 100 degrees F inlet and running in a 115 degree foundry loses capacity and runs closer to its high-temp trip all the time. If the room runs hot, either duct the intake somewhere cooler or go water-cooled. More on room setup in air compressor room requirements.
The Silica Rule, and Why It Touches Your Air System
OSHA's respirable crystalline silica standard for general industry, 29 CFR 1910.1053, sets a permissible exposure limit of 50 micrograms per cubic meter as an 8 hour time weighted average, with an action level of 25 micrograms per cubic meter. Cross the action level for 30 or more days a year and workers go into medical surveillance at your expense.
Compressed air shows up in that conversation in two ways, and both are ways foundries get written up.
Blowing down with compressed air. Using an air wand to clean sand off a mold, a casting, a bench or a worker's clothes takes settled silica and puts it straight back into the breathing zone. The standard restricts dry methods where feasible alternatives exist, and inspectors know exactly what a blow-off station looks like. Vacuum with HEPA, or wet methods, are the defensible answer. Where blow-off genuinely cannot be avoided, OSHA's general requirement still caps air used for cleaning at 30 psi at the nozzle with effective chip guarding and PPE.
Supplied air respirators. Cleaning room and blast operators are often on airline respirators, and the moment you feed a respirator from your plant compressor you are on the hook for Grade D breathing air per CGA G-7.1, including a carbon monoxide alarm or monitor if the source compressor is oil-lubricated. That is a whole filtration train, not a filter. We laid it out in Grade D breathing air requirements.
Air Quality Targets
Foundries do not need pharmaceutical air. They need air that will not rust out a system and will not destroy pneumatic tools.
| Use | Target | What that takes |
|---|---|---|
| Rammers, chippers, general tools | Dry enough to stop rust, lubricated at the tool | Refrigerated dryer plus general purpose filter, FRL at the drop |
| Core blowing | Dry. Moisture in core sand is a defect. | Refrigerated dryer minimum, desiccant if lines run outdoors |
| Molding machine actuation | Clean and dry | Same as general plant air |
| Blast and cleaning room | Dry, high volume | Dryer sized for the real blast load, which is usually bigger than anyone planned |
| Supplied air respirators | CGA G-7.1 Grade D | Dedicated filtration train plus CO monitor on oil-lubed sources |
Wet air in a foundry is worse than in most plants because of core sand. Moisture in the blow air changes how the sand packs and how the binder cures, and you get soft cores and scrap castings with no obvious cause. A refrigerated dryer is the baseline. Go desiccant if any part of the header runs through unheated space.
Sizing, Honestly
Do not add up nameplates. Foundry equipment lists overstate demand badly because nothing runs continuously at nameplate except the cleaning room.
The approach that works:
- Meter the existing system for a full production week if you have one. A flow meter on the header for seven days tells you more than any calculation.
- Separate spike demand from base demand. Core blowing and shakeout are spikes, handled with storage. Cleaning room and rammers are base, handled with horsepower.
- Size the compressor on base plus average spike contribution, then add 25 to 30 percent.
- Plan for two machines, not one. Foundries run hot and dirty and compressors there fail more often than the catalog MTBF suggests. A second machine is not luxury, it is the difference between a bad afternoon and a cold cupola.
- Look hard at VSD on the lead machine. Foundry demand between pours and during shift change swings a lot, and an unloaded fixed speed screw still eats 20 to 35 percent of full load power. See control modes compared.
Most small to mid-size foundries land on 50 to 200 HP total in rotary screw compressors, split across two or three machines, with 1,000 gallons or more of distributed storage. Large production foundries go well past that.
What Foundries Get Wrong
- Chasing core blow dips with horsepower. It is a storage problem. Adding a machine treats the symptom at the worst possible price.
- Leaving the compressor breathing plant air. The cheapest reliability upgrade in the building is a duct.
- Cleaning room on the same header as everything else. A blast cabinet that pulls 150 CFM continuously will flatten pressure for the whole plant. Either give it its own machine or give it its own storage and a properly sized branch.
- Black iron everywhere. Wet air plus steel pipe equals rust, and rust in a core blower nozzle is a scrapped core. See pipe materials compared.
- Treating air wands as a cleaning method. Covered above. It is a silica citation waiting to happen and it is also enormously wasteful. Engineered nozzles help where blow-off is unavoidable.
- No leak program. Foundries are hard on hose, fittings and couplers. A plant that has never done a leak survey is typically losing 25 to 35 percent of its output. Start with leak detection.
Frequently Asked Questions
Why does my compressor keep overheating in the summer?
In a foundry, usually a plugged cooler face or a restricted intake filter, not a refrigerant or fan problem. Plant ambient is already high, so the machine has very little thermal margin, and a dust-packed cooler removes what margin was left. Pull the cooler, clean it properly, duct the intake, and check the trip history again.
Do I need oil-free air for core blowing?
No. Core blowing needs volume and dryness, not oil-free purity. A well-maintained oil-lubricated rotary screw with a proper separator and coalescing filter is fine. Spend the money on storage and drying instead.
Can I run supplied air respirators off my plant compressor?
Only if you build the system to deliver CGA G-7.1 Grade D air, which means a dedicated filtration train and, on an oil-lubricated source compressor, a carbon monoxide alarm or continuous monitor. Many foundries find a dedicated breathing air compressor simpler than qualifying the plant system.
How do I stop pressure dipping every time the core blowers fire?
Put a receiver near the core room, feed it through a flow restrictor so it refills slowly instead of pulling from the header, and let it absorb the shot. This is far cheaper than more horsepower and it works immediately.
Is compressed air blow-off a silica violation?
Using compressed air to clean settled silica dust off surfaces, castings or clothing re-entrains it into the breathing zone, and OSHA expects you to use vacuum with HEPA or wet methods where feasible. Where blow-off genuinely cannot be avoided, air used for cleaning is still limited to 30 psi at the nozzle with effective guarding and PPE.
What size compressor does a small jobbing foundry need?
Meter first, but a small jobbing shop with a couple of molding machines, a core blower and a modest cleaning room commonly lands somewhere in the 50 to 100 HP range with generous distributed storage. The cleaning room is usually the number that surprises people.
Get compressed air for foundries right and you fix three problems at once: compressors that stop dying early, core scrap that stops appearing for no reason, and a silica exposure story you can actually defend. Start with the intake duct and the core room receiver. Those two are cheap and they move the needle more than another machine will.


