


The call usually comes in around the middle of second shift. A weld cell faulted, a clamp let go a half second early, and the line stopped. Nobody tripped a breaker and nothing broke. The plant air sagged for a few seconds when a wash station and a bank of nutrunners all asked for air at once, and the cell read it as a fault. That is the daily reality of compressed air for automotive parts manufacturing. The air itself is not exotic. What makes it hard is that the plant is judged by the minute, and the air touches almost every one of those minutes.
We sell to a lot of Tier 2 and Tier 3 suppliers, the shops stamping brackets, machining housings, assembling sub-modules and molding trim for the bigger names. This piece is written for them. If you run a full vehicle assembly plant with a utility group and an energy manager, you already have people for this. If you are the maintenance lead or plant manager at a supplier doing a few hundred thousand parts a week, read on.
Why a Parts Supplier Is Not Just Another Shop
A general fabrication shop can live with a bad afternoon of air. A supplier on a customer's schedule cannot. Automotive programs run on takt time, and a stopped line costs you in ways that show up on a chargeback sheet. Your customer also audits you. Most suppliers in the chain work under IATF 16949, the automotive quality management standard, and that means documented processes, preventive maintenance records, and a corrective action trail when something goes wrong. Air does not appear by name in that standard, but a recurring air problem that causes scrap or downtime is exactly the sort of thing an auditor asks about.
The other difference is variety. One building often has a weld cell, an assembly line, a test stand, a parts washer, a coating booth and a maintenance shop, all on one header. Each of them wants something different from the same air.
Where the Air Actually Goes
Walk the floor and you will find air in roughly six places.
- Fixtures, clamps and robot tooling. Pneumatic clamps, grippers and cylinders hold parts in weld, machining and assembly cells. These care a great deal about steady pressure and dry air. A dribble of water in a small valve causes sticking, and sagging pressure causes slow or weak clamping.
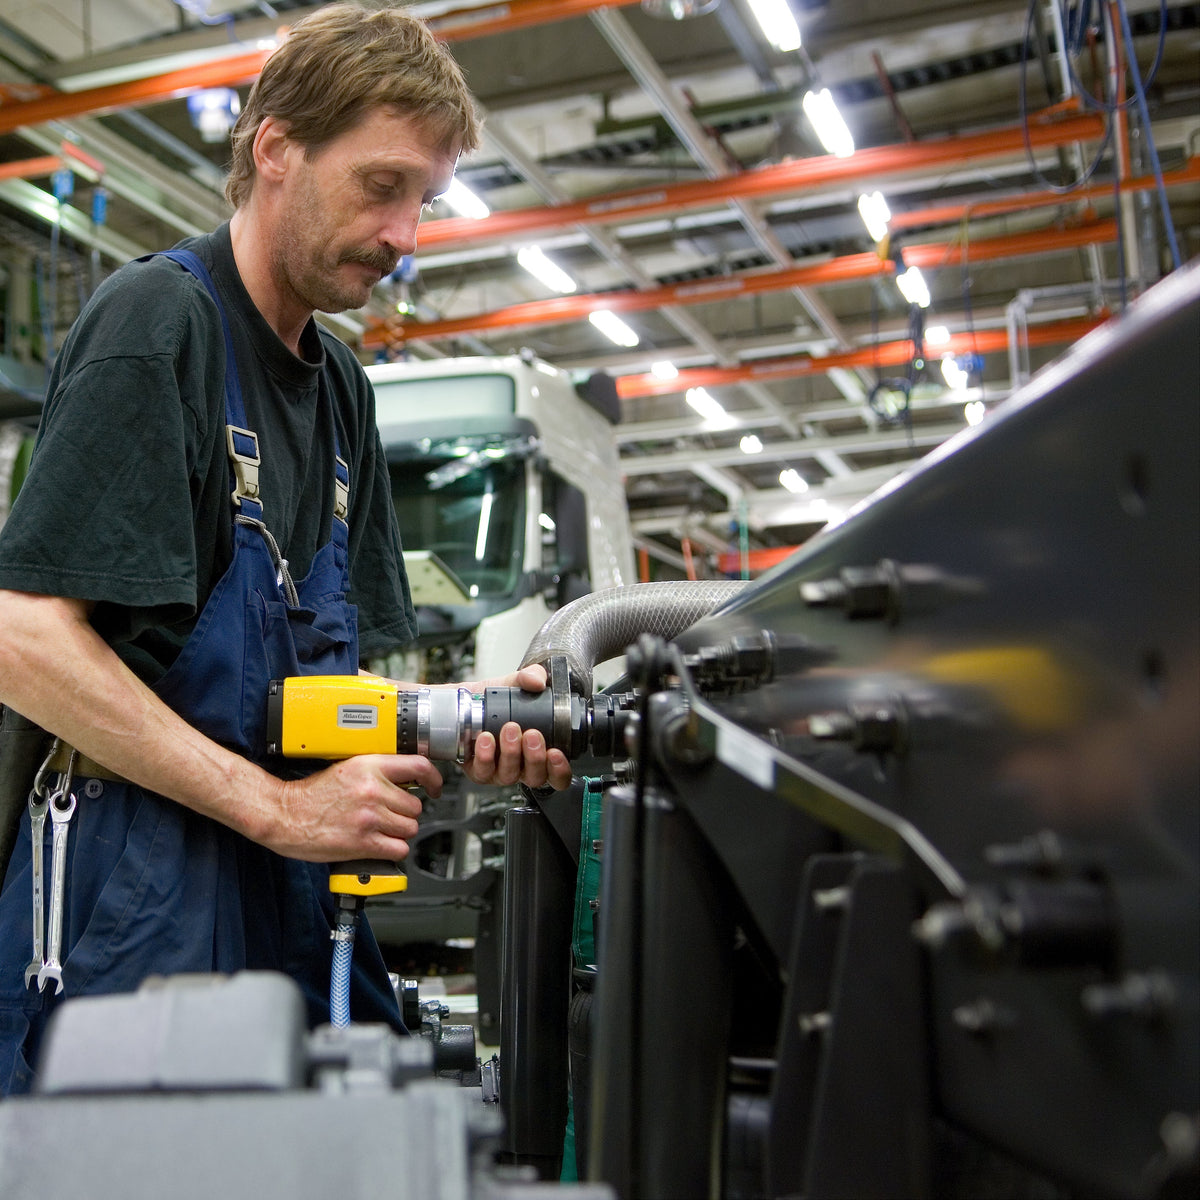
- Assembly tools. Pneumatic nutrunners, screwdrivers, impact wrenches and torque tools. Most tool makers rate these around 90 psi at the tool. Our air tool CFM chart shows what the common ones draw.
- Leak and functional testing. Fuel rails, cooling components, housings and sealed assemblies get pressure tested. Test stands are sensitive to supply pressure swings and to moisture, because a drifting supply looks like a leak and you get false rejects.
- Blow-off and cleaning. Removing chips and coolant from machined parts, drying washed parts, cleaning fixtures. This is the biggest source of wasted air in most plants, and it is usually done with open pipe or a cheap blow gun.
- Coating and paint. Atomizing air for spray, powder or e-coat adjacent lines. This is the one with the strictest quality requirement.
- Maintenance and general use. Blow guns, hose drops, the tool crib, tire and cart service.
Here is a rough picture of where a typical plant's air gets used, from a sample load breakdown published by an industrial monitoring vendor: production tools and robots around 46 percent, leaks around 24 percent, open blowing around 14 percent, and paint and process air around 10 percent. That split is an illustration, not a measurement of your plant, but the pattern is familiar. Production air is roughly half. The rest is waste you can go after.
Air Quality by Zone, Not by Plant
The mistake we see most is treating the whole plant as one air quality. You end up either overspending to make every drop paint-grade, or underspending and fighting defects in the one place that matters. A better plan is to treat the main header to a sensible standard and add point-of-use treatment where the process demands it.
ISO 8573-1 is the yardstick. If you need a refresher, our ISO 8573-1 classes explainer decodes the three numbers. For orientation, humidity class 4 means a pressure dew point at or below 37 degrees F (3 degrees C), class 3 is minus 4 degrees F (minus 20 C), and class 2 is minus 40. Oil class 1 allows no more than 0.01 mg per cubic meter of total oil, and class 0 is whatever tighter figure you and your supplier agree to and can prove.
| Zone | What matters | Typical treatment |
|---|---|---|
| General plant header, tools, blow-off | Bulk water and rust out, steady pressure | Aftercooler, refrigerated dryer, particulate filter, zero-loss drains |
| Fixtures, clamps, cylinders | No water, no oil carryover that gums valves | Refrigerated dryer plus coalescing filter, regulator at the cell |
| Leak and functional test | Stable pressure, dry air, no drift | Dedicated branch, point-of-use filtration, local receiver or flow controller |
| Coating and paint | Oil-free and, where specified, silicone-free | Desiccant dryer, coalescing and adsorption filters at the booth, certified components |
| Plant instruments and controls | Dry and clean, outdoor lines do not freeze | Desiccant dryer on the instrument branch |
The Paint and Coating Line Deserves Its Own Paragraph
Paint shops use the term LABS, short for paint wetting impairment substances, for anything that makes a coating pull away from the surface and leave craters. Silicone and oil are the usual suspects. Compressor oil in the air is one of the ways it gets there, which is why paint-bound air is oil-free or filtered very tight, and why a lot of OEM specs add a silicone-free requirement for everything in the air path, including seals and lubricants in filters and regulators.
Here is where we want to be straight with you. If your customer specifies LABS-free or silicone-free air, get that requirement in writing and ask the manufacturer of every component in that branch to confirm it. We can tell you what the manufacturer documents for a given oil-free compressor or filter housing. We will not guess, and you should not take a salesperson's word for it. A single wrong lubricant in a regulator can undo the whole branch.
For the spray line, treat the booth branch as its own system. A desiccant dryer to get the dew point down, coalescing filtration, an adsorption stage for oil vapor, and a final filter close to the gun. The Nano purification line covers the filters, adsorption stages and desiccant dryers for this kind of branch.
Sizing the Compressor Room
A supplier's demand is lumpy. A press or a washer cycles on and off, a test stand pulls a surge, and three shifts mean the load never fully rests. Two numbers drive the sizing. The first is your measured peak flow, not the sum of every nameplate. Our piece on diversity factor explains why adding up every tool buys too much compressor. The second is your growth. Suppliers add cells when a new program lands, and an air system sized to the day it was installed is already short.
A common rule of thumb for rotary screw compressors is about 4 CFM per horsepower at 100 psi. So a plant that measures 160 CFM at peak and wants 25 percent headroom for growth lands near 200 CFM, which is around a 50 HP machine. Treat that as arithmetic to get started, not a quote. Your actual number comes from a flow meter or a load and unload log on the machine you have.
Two other habits pay off in this industry.
- Two machines, not one big one. A single large compressor is a single point of failure. Two machines sized to share the load, with lead and lag control, means a failure slows you down instead of stopping you. We cover the idea in what happens when your only compressor goes down.
- A variable speed machine for the trim. If your demand swings between first shift and a skeleton third shift, a VSD unit handling the variable part of the load saves real energy compared with a fixed speed machine unloading and idling.
Storage, Pressure and the Leak Problem
The fault that opened this article is a storage and pressure problem. Add wet receiver capacity ahead of the dryer to buffer the compressor, and dry receiver capacity after the dryer near the big intermittent users. For a cell that is sensitive to dips, a pressure flow controller after a receiver lets the cell see a steady downstream pressure while the receiver absorbs the surge. We explain the idea in our pressure flow controller guide.
Then there is the cost of pressure. A US Department of Energy rule of thumb says every 2 psi of extra discharge pressure adds roughly 1 percent to compressor energy use. Plants raise pressure to cover for a bad pipe run or a starved cell, and then pay for it on every tool in the building. Fix the restriction, then lower the setpoint.
Leaks are the other quiet cost. The Compressed Air Challenge reports that a poorly maintained system can lose 20 to 30 percent of compressor output to leaks, and a well maintained one stays under 10 percent. A Sunday test tells you a lot. With production stopped, whatever your compressors are still producing is your leak and idle demand.
Piping the Floor
Supplier floors get rearranged. Cells move, a new line goes in, a fixture changes. Hard-to-modify black iron fights you. Aluminum pipe goes in fast, stays clean inside, and is easy to extend. Run a loop around the building rather than a dead-end line, size it for the flow you will have in three years, and drop from the top of the main so condensate does not run down into a clamp valve. Our pipe sizing guide has the numbers.
What We Sell and What We Don't
We sell the air system: rotary screw and piston compressors, refrigerated and desiccant dryers, filters, drains, receivers, piping and breathing-quality purification. We do not sell robots, nutrunners, test stands, leak testers or coating equipment, and we are not going to tell you which brand of weld cell to buy. What we can do is help you match a compressor and treatment train to the load you measured, and tell you what each filter and dryer is rated for so you can write it into your own control plan.
Mistakes We See in Supplier Plants
- One header, one quality. Either the paint line gets bad air or the whole plant gets expensive air.
- Blow-off with open pipe. Replace it with engineered nozzles and a solenoid so air only flows when a part is present.
- No flow meter. If you cannot say what the plant uses on a Sunday, you cannot prove an improvement.
- No backup. The plant that runs one compressor learns what it costs on a Tuesday night.
- Raising pressure to cover a pipe problem. The energy bill pays for it forever.
- Putting the compressor room in the dirtiest corner. Chips, coolant mist and heat all go into the intake. See our compressor room requirements.
If you are replacing an aging machine or adding capacity for a new program, start with the rotary screw compressors and size the treatment train around the zones above.
Frequently Asked Questions
What air quality does an automotive parts plant need?
It depends on the zone. General tool and blow-off air usually does fine with a refrigerated dryer and a particulate filter. Clamp and cylinder branches benefit from a coalescing filter too. Paint and coating branches need oil-free air and often silicone-free components, and your customer's specification is what decides the exact class.
Do I need an oil-free compressor for a paint line?
Not always. Many plants use an oil-injected compressor with a well maintained coalescing and adsorption train at the booth. Others choose oil-free to remove the oil source entirely. Either can work, but check what your coating specification and customer require and keep the filter change records.
How big a compressor does a small supplier need?
Measure first. As a starting rule, rotary screw machines deliver about 4 CFM per horsepower at 100 psi, so a plant peaking at 160 CFM with growth headroom lands around a 50 HP unit. Two smaller machines sharing the load give you redundancy that one large one cannot.
Why do my test stands give false rejects?
Often it is the supply. Pressure swings and moisture make a stable part look like it is leaking. A dedicated branch with local storage or a pressure flow controller, plus dry filtered air, is the usual fix.


